
CALL US TODAY OR WHATSAPP
+86 13423121371
info@dgvimsteel.com

1.2714 hot work tool steel is a hot work tool steel with high impact strength, ductility, very good hardenability, high resistance to high temperatures and temperature differences that occur during operation. They are also alloy materials used in the metallurgical industry where high mechanical properties are also required and low deformation tendency during heat treatment is required.
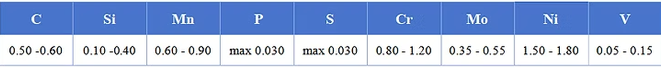
Chemical Composition
Forging
Preheat slowly to 700ºC then increase temperature more rapidly to 1050ºC. Do not forge below 800ºC. It isessential to cool slowly after forging, either in a furnace or in vermiculite.
Annealing
Soak thoroughly at 740-760ºC before furnace cooling at a maximum rate of 10ºC per hour down to 600ºC followed by cooling in air.
Stress Relieving
When tools made from 1.2714 steel are heavily machined or ground, the relief of internal strains isadvisable before hardening to minimise the possibility of distortion. Stress relieving of this grade shouldbe done after rough machining. To stress relieve, heat the component carefully to 600-650ºC, allow a goodsoaking period, about two hours per 25mm of section. Cool in the furnace to 500ºC then freely in air. Tools may then be finish machined before hardening.
Hardening
Pre-heat at 650ºC followed by rapid increase of temperature to the hardening temperature of 900-950ºC. Quench in oil.
Heat Treatment
Heat treatment temperatures, including rate of heating, cooling and soaking times will vary due to factorssuch as the shape and size of each 1.2714 steel component. Other considerations during the heattreatment process include the type of furnace, quenching medium and work piece transfer facilities. Please consult your heat treatment provider for full guidance on heat treatment of 1.2714 tool steel.
